HomeHow Scaffolding Is Made: Our Production Steps
How Scaffolding Is Made: Our Production Steps
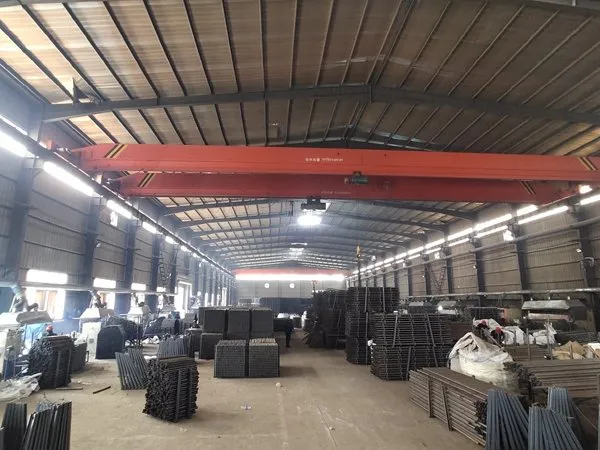
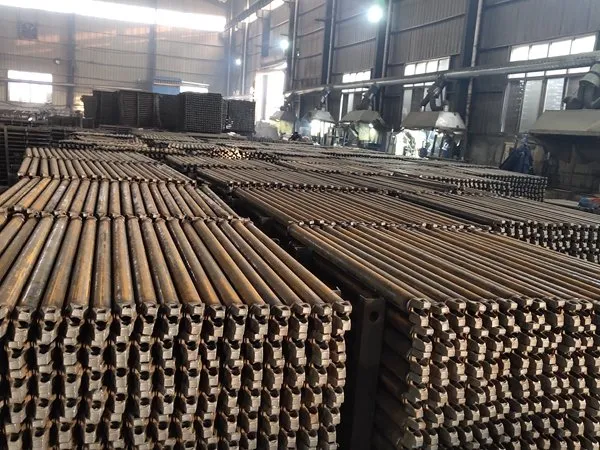
We build scaffolding with a mix of automatic lines and skilled hands. Here is the path a standard takes from steel tube to finished product.
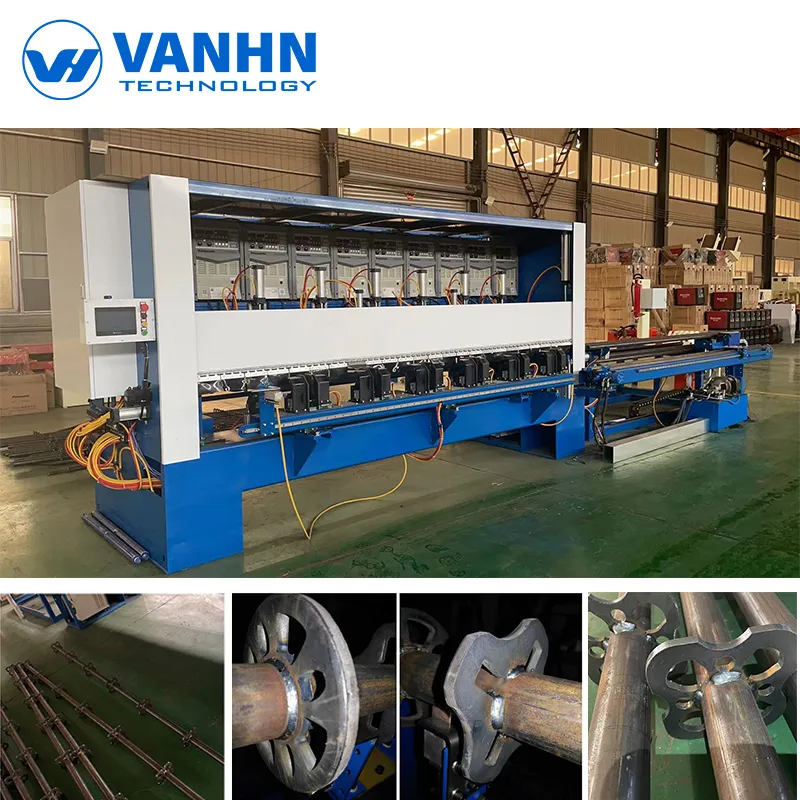
Standards line, as it runs
| Step | What happens |
|---|---|
| 1. Tube cutting | Laser tube cutter feeds and cuts to length |
| 2. Punching | Both tube ends punched in one stroke |
| 3. Rosette placing | Rosettes set on the tube at 500 mm pitch |
| 4. Welding | 13 welding power sources weld every rosette at once, MAG/CO2 gas shielded |
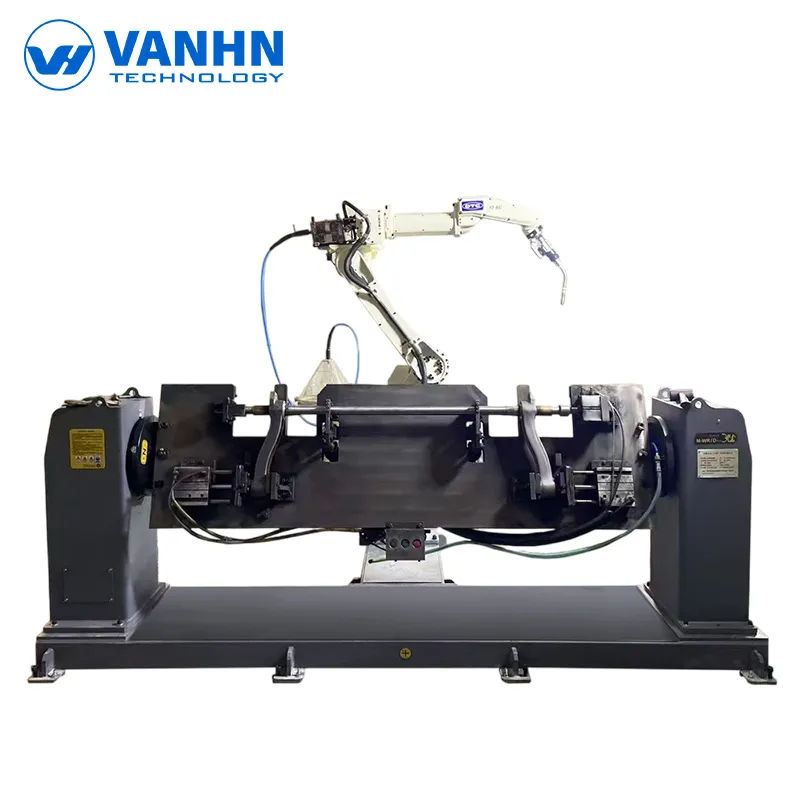
| 5. Stacking | Robot arm stacks finished standards |
Output of the standards line: 3,500 pieces per 10 hours in the 1+4 layout.
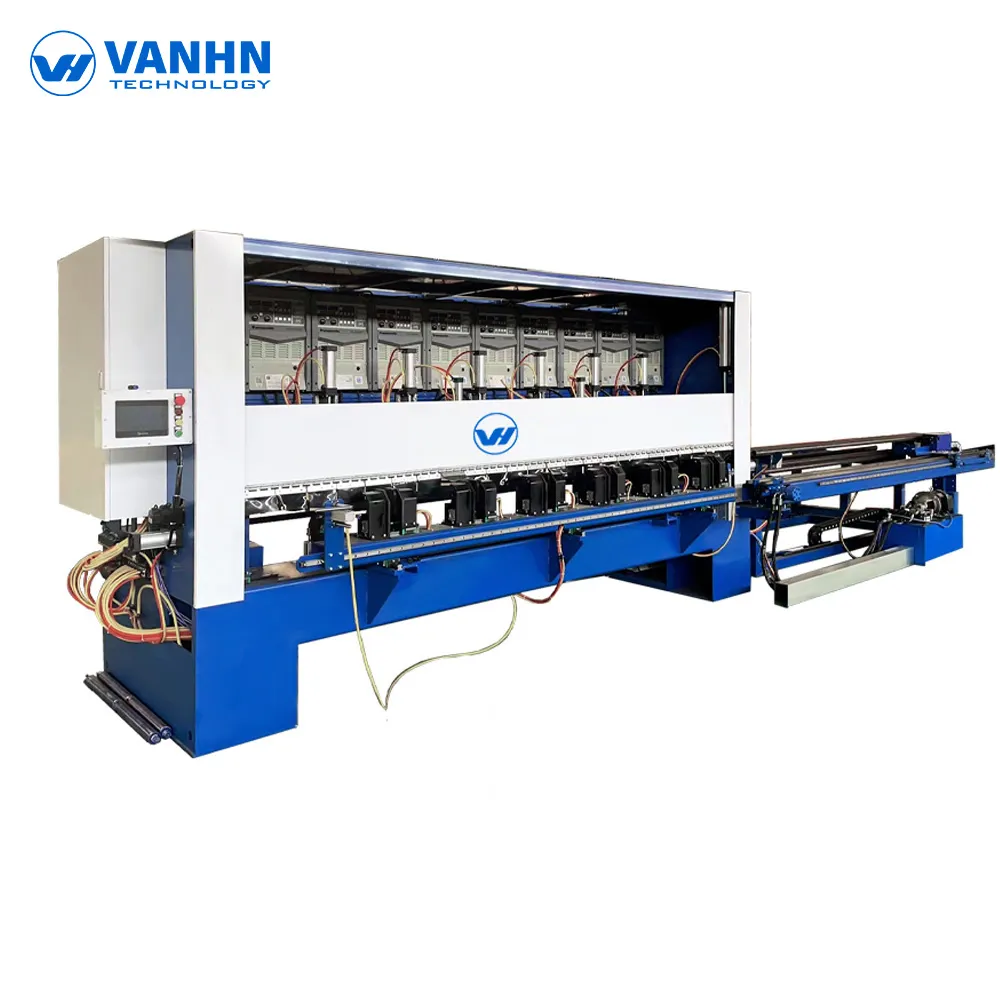
How We Build a Standard
- Laser tube cutting. Steel tube enters the line and is cut to length with a laser. This gives clean edges and repeatable sizes.
- Punching. The tube is punched to create the holes where rosettes and other parts will fit.
- Rosette placing. A rosette is positioned on the tube at the right spacing, ready for welding.
- Automatic welding. Thirteen welding power sources work at once on the standard welding machine. The process is MAG/CO2 gas-shielded welding.
- Robot stacking. Finished standards are stacked by a robot, which keeps the line moving and reduces manual handling.
Ledgers and Braces: Welding and Punching
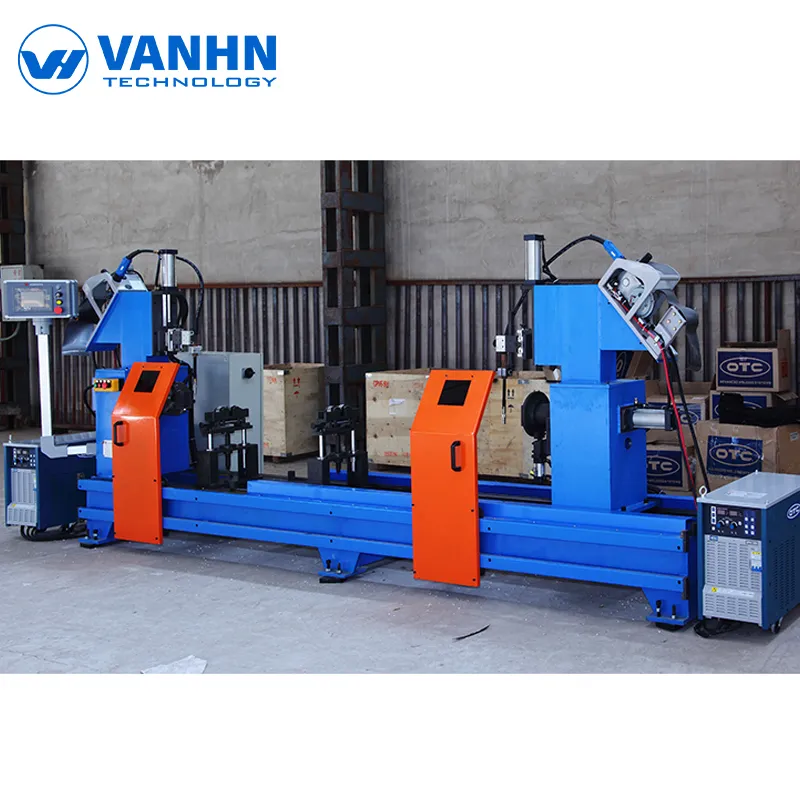
Ledger welding uses dual torches, so both ends are welded together in one pass. This helps keep the ledger ends aligned and the weld consistent. Our ledger line handles tube from 0.3 to 3.2 meters, depending on the machine.
Braces go through a press-and-punch process. The machine works with tube diameters of 33, 42, and 48 mm and wall thickness from 2.5 to 3 mm. It can produce 360 to 500 pieces per hour, which lets us keep brace supply in step with the rest of the system.
Steel and Finish: Q355, Q235, Galvanizing
We use Q355 steel for standards because they carry the main load. Ledgers, braces, and planks are made from Q235. This split keeps strength where it matters and cost down where it does not.
Most components are hot-dip galvanized. That finish gives a service life of 15 years or more. If a project needs a different look, we can paint or powder coat parts in red, orange, blue, or yellow. The choice depends on the site and the buyer's preference.
Tell us what you are building
Say what failed you last time. We answer with specifics, not a brochure.
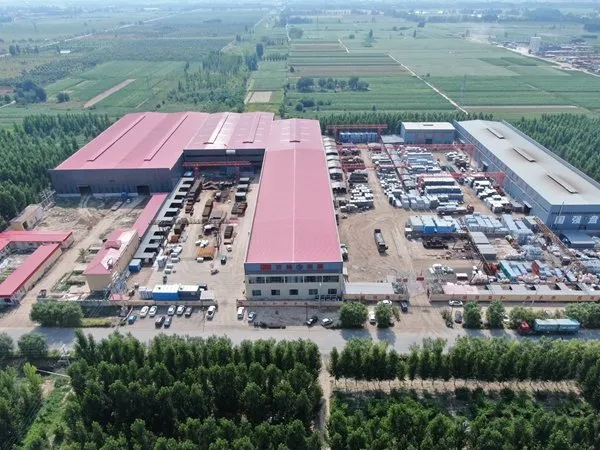
- Made in our own plant, 100,000 m², founded 2016
- Hot-dip galvanized, painted or powder coated
- Reply within 24 hours